Bags are not apparel, and that decides which factory you should contact. A bag line works with heavier fabrics, heavier machines and a long list of hardware: webbing, buckles, D-rings, grommets and zips. The factory that sews your t-shirts is rarely set up for it.
This guide profiles seven bag manufacturers in the USA, China and India and says what each one states on its own website, including the minimums they publish. It is an editorial list, not a ranking and not a list of our partners. It then covers what to decide before you contact anyone, what a bag tech pack needs and how to check a maker.
Heads up: We're Portugal Clothing Factory. Our team places and manages clothing production with partner factories in northern Portugal. We don't make bags, and none of the companies below is one of our partners; we have no commercial relationship with them.
Key Takeaways
- Bag making is its own discipline. Heavier fabrics, heavy-duty machines and a hardware list most clothing factories don't keep.
- Seven makers profiled: Unionwear, Fieldtex Cases, Tough Traveler and John Boyt in the USA, Quanzhou Osgoodway and DANKIN in China, and Optima Bags in India.
- Published minimums vary widely: from no minimum (Fieldtex) to 100 per model (Optima) and 500 per style and colour (Osgoodway).
- Volume comes from Asia: China, Cambodia and Vietnam supplied 71% of US handbag imports by units in 2024 (IndexBox).
- Decide the bag type first. A tote, a laptop backpack, a tactical case and a leather handbag each need a different kind of maker.
Why Can't an Apparel Factory Make Your Backpack?
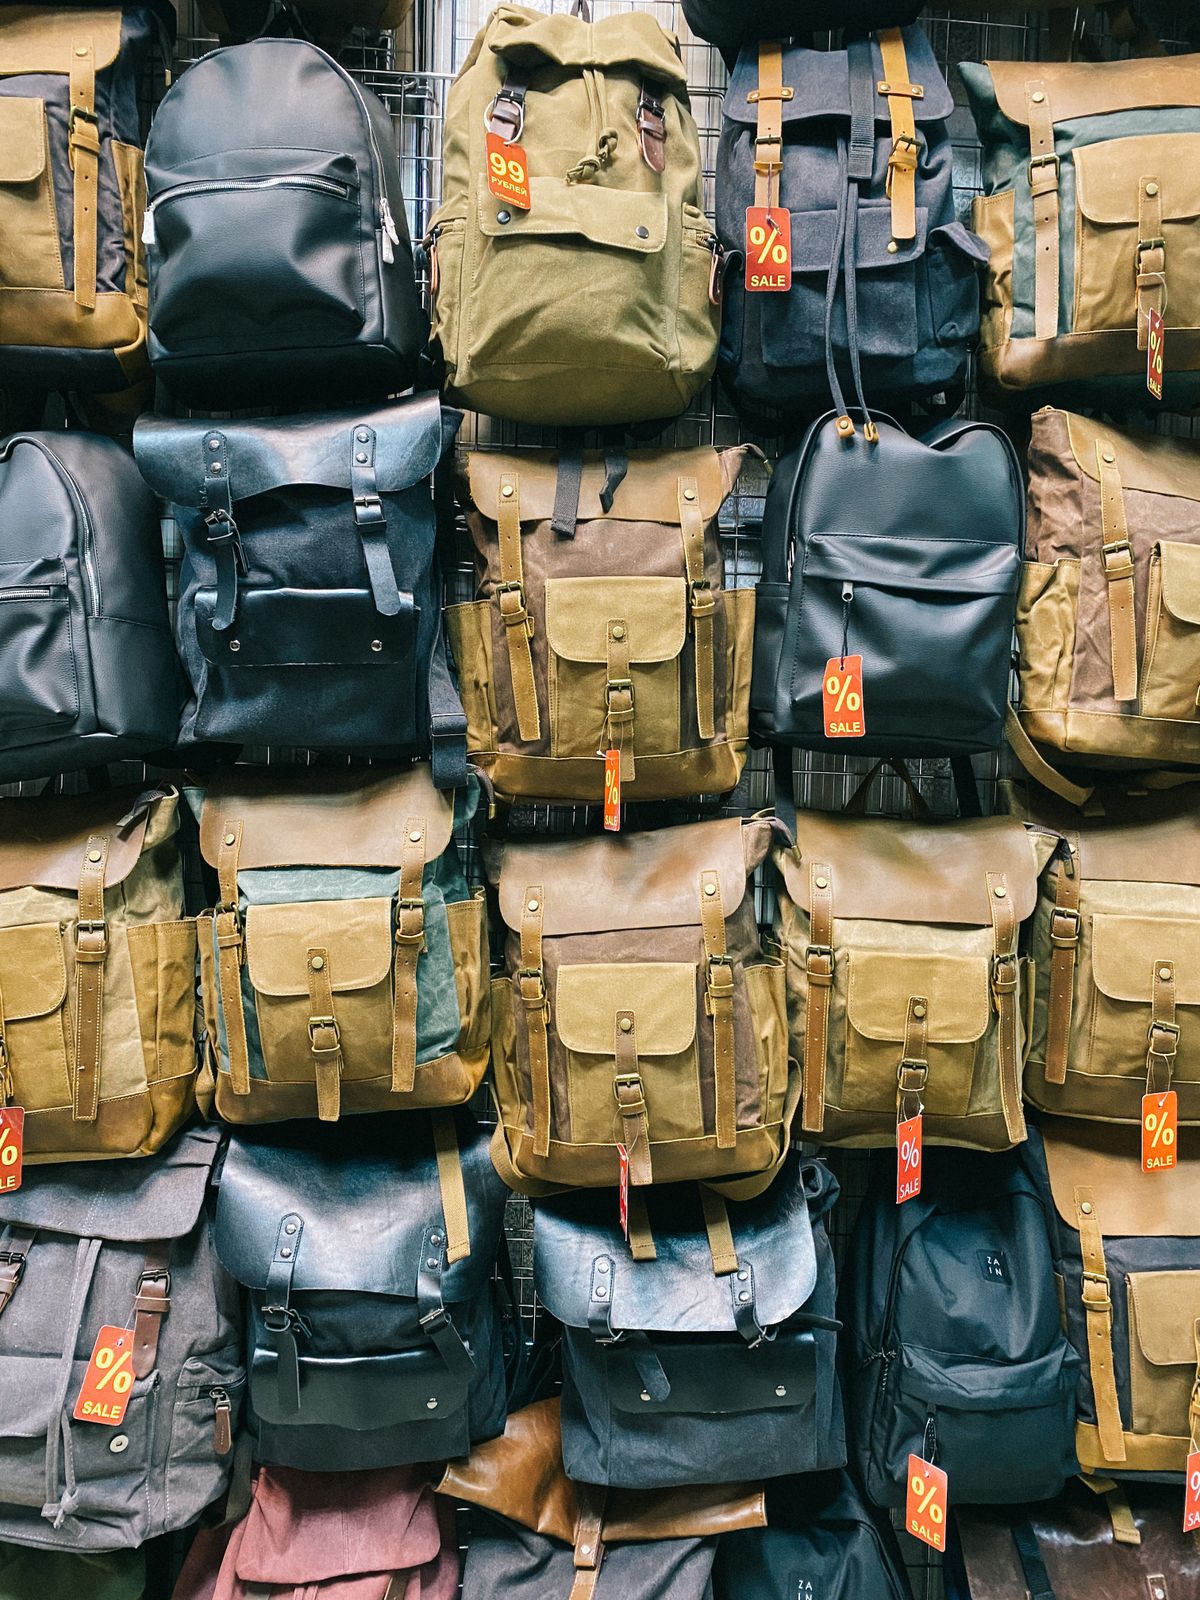
Because the machines, the materials and the bill of materials are different. A clothing line is set up for knits and light wovens, with lockstitch, overlock and coverstitch machines. A bag line feeds thick, coated or technical fabrics such as 1000D Cordura, ballistic nylon, 600D polyester and heavy canvas through heavy-duty and walking-foot machines.
Then there is the hardware. The custom bags page of John Boyt Industrial Sewing lists stainless steel grommets, D-rings and snaps, acetal buckles and tri-glides, heavyweight webbing, RF welding, heat sealing and die cutting. A garment bill of materials has almost none of that. If a clothing supplier happily accepts a bag order, ask whether the bag will be made on its own premises or sent to another plant.
Citation Capsule Bag manufacturing and apparel cut-and-sew are separate disciplines. Bag makers run heavy-duty and walking-foot machines for fabrics such as 1000D Cordura, ballistic nylon and heavy canvas, and their bill of materials includes webbing, grommets, D-rings, buckles and zips. Clothing lines are set up for knits and light wovens and usually carry neither the machines nor the hardware.
Which Type of Bag Are You Making?
Answer this before you contact anyone, because "bag manufacturer" covers very different factories. A promotional tote and a technical hiking pack share a word and little else: different fabric weights, machines, panel counts and checks. Complexity here means the number of panels, the amount of hardware and the number of separate operations, which is what drives price and minimum.
| Bag type | Typical build | Complexity | Look for a maker that lists |
|---|---|---|---|
| Promotional tote | Canvas or non-woven, few panels, little or no hardware | Low | Totes, printing or embroidery |
| Drawstring bag | Light polyester or nylon, cord, minimal stitching | Low | Drawstring bags, logo printing |
| Laptop backpack | Padded panels, foam, zips, moulded hardware | High | Laptop bags, padding, own sample room |
| Technical outdoor pack | Cordura or ripstop, load-bearing webbing, bar-tacks | High | Hiking or outdoor packs, strap and seam testing |
| Tactical or medical case | 1000D Cordura, mil-spec webbing, documentation | High | Military or medical work, quality certification |
| Leather handbag | Cut leather, hand finishing, edge painting | High | Leather goods, not textile bags |
| Cooler or insulated bag | Insulation layers, welded or heat-sealed seams | Medium | Cooler bags, RF welding or heat sealing |
Indicative guide built from the capability pages of the makers profiled below. Not an exhaustive map.
How Did We Choose These Manufacturers?
We started from the companies in our earlier research and checked each one on its own website in October 2026. We kept makers whose own site describes custom or private-label bag production, and we dropped three whose sites no longer showed it: one is now a consumer shop, one a consumer brand page and one a site under construction. We did not rank the seven that remain.
Factory size, capacity, certifications and minimums below are what each company says about itself. They are not independent audits, so ask for certificate numbers and check them before you commit.
Who Are the Leading US Bag Manufacturers?
Unionwear (Newark, New Jersey)
Unionwear makes union-made custom accessories, including backpacks, totes and drawstring bags, and has been in business since 1992. Its backpacks page says its bags are "100% custom made in USA" at its Newark factory, with wholesale pricing for branded orders. It does not publish a bag minimum on that page, so ask.
Fieldtex Cases (Rochester, New York)
Fieldtex is a contract sewing manufacturer of tactical bags, military-grade backpacks, soft-sided cases and medical and EMS bags. Its military-grade sewing page states US-based sewn product manufacturing since 1973, an ISO 9001 certified facility, an 86,000 square foot production floor with more than 125 operators, and Berry Amendment compliant production. Its contact panel states "no minimum order quantities".
Tough Traveler (Schenectady, New York)
Tough Traveler makes backpacks, luggage and cases and offers custom design, prototyping and manufacturing. Its custom design page says it has made bags in the USA since 1970 with all production in-house, works from a single prototype to runs of thousands, and usually needs ten or more pieces for silkscreen or embroidery. It quotes prototype costs from $100 to $10,000, with most projects between $500 and $1,500, and stocks Packcloth, Cordura, vinyl, webbing and YKK zips.
John Boyt Industrial Sewing (Urbandale, Iowa)
John Boyt is a contract industrial sewer rather than a bag brand, with more than 45 years in business. Its custom bags page describes padded, carry, equipment and fire-resistant bags on a cut-only, labour-only or full cut-and-sew basis, in vinyl, canvas, polyester, Cordura and ballistic fabrics, with RF welding, die cutting and grommet setting. The example on that page lists a volume of 50 and up and a three-week average turnaround.
Citation Capsule The made-in-USA bag field is small but real. Unionwear (Newark, New Jersey) makes custom union-made bags; Fieldtex Cases (Rochester, New York) makes tactical and medical bags and states no minimum order quantities; Tough Traveler (Schenectady, New York) has made bags in the USA since 1970; John Boyt (Urbandale, Iowa) sews custom bags on contract. Figures are self-reported.
Who Are the Leading Bag Manufacturers in China?
Quanzhou Osgoodway (Nan'an, Fujian)
Osgoodway is an OEM and ODM maker of backpacks, duffels, hiking and sports bags, cooler bags and bags made from recycled materials. Its about page states it has exported since 2014, runs an 8,600 square metre factory with more than 100 workers and makes around 100,000 units a month. It also says it works with a network of more than ten partner manufacturers alongside its own facility, so ask where your style will be sewn. Standard OEM orders start from 500 pieces per style and colour, and higher for custom-dyed materials, own hardware or complex builds. It lists BSCI, GRS and ISO 9001:2015 and quotes 7 to 10 days from sketch to sample.
DANKIN Light Industrial (Quanzhou, Fujian)
DANKIN makes backpacks, sports, outdoor, travel, laptop and cooler bags and fashion handbags, and says 90% of its orders are OEM or ODM. On its website it states it was founded in 1991, runs four production lines with around 320 workers, and has passed BSCI, SEDEX, GRS, SA8000 and ISO 9000 audits among others. For a custom logo it gives a minimum of 25 pieces up to 500 or 1,000 depending on the design, so the low end applies to simpler bags.
Who Are the Leading Bag Manufacturers in India?
Optima Bags (Kundli, Haryana, near Delhi)
Optima makes backpacks, school bags, duffels, luggage and totes for export buyers and private-label brands. Its about page says it was founded in 1995 as a watch manufacturer and moved into bags and cases in 2010, and that its main factory is in Kundli, Haryana, with a 40,000 square foot floor and about 100,000 bags a month. It lists ISO 9001:2015, ISO 14001 and ISO 45001 and a SEDEX audit. Its backpack manufacturing page states a standard minimum of 100 pieces per model.
Here is how the seven compare at a glance.
| Manufacturer | Location | Focus | Published minimum |
|---|---|---|---|
| Unionwear | Newark, NJ, USA | Union-made custom bags and accessories | Not published for bags |
| Fieldtex Cases | Rochester, NY, USA | Tactical, medical and industrial bags | No minimum stated |
| Tough Traveler | Schenectady, NY, USA | Backpacks, luggage, custom development | From one prototype; 10+ for decoration |
| John Boyt | Urbandale, IA, USA | Contract industrial sewing | Example lists 50+ |
| Quanzhou Osgoodway | Nan'an, Fujian, China | Backpacks, duffels, recycled bags | 500 per style and colour |
| DANKIN | Quanzhou, Fujian, China | Wide OEM range, cooler bags | 25 to 1,000 by design |
| Optima Bags | Kundli, Haryana, India | Backpacks, luggage, private label | 100 per model |
Source: each company's own website, checked October 2026. Size, capacity and certifications are self-reported.
Where Are Bags Actually Manufactured?
By volume, mostly in Asia; by value, the picture changes. According to IndexBox, the United States imported 246 million units of handbags worth $3.9 billion in 2024. China (93 million units), Cambodia (50 million) and Vietnam (17 million) supplied a combined 71% of that volume.
By value the order flips: Italy led at $1.2 billion, ahead of Cambodia at $595 million and China at $382 million. Leather goods carry a far higher price per unit than mass-market nylon. If your product is a leather handbag, you are looking at a different set of makers from someone making a 600D polyester backpack.
| Supplier | US handbag imports 2024 |
|---|---|
| China | 93 million units |
| Cambodia | 50 million units |
| Vietnam | 17 million units |
| Italy (by value) | $1.2 billion |
| Total | 246 million units, $3.9 billion |
Source: IndexBox, Handbags United States market overview 2024.
What Is the MOQ Reality for Custom Bags?
There is no standard minimum. Among the seven makers here, Fieldtex states no minimum, Tough Traveler starts from a single prototype, Optima states 100 pieces per model, Osgoodway 500 pieces per style and colour, and DANKIN 25 to 1,000 depending on the design. Unionwear and John Boyt quote per project.
Treat a very low published figure with care. A minimum of 25 is likely to apply to a simple bag with your logo on it, not a new pattern with custom hardware. Branded buckles, zip pulls and moulded parts can carry their own minimums and tooling costs, so ask the maker to show tooling separately from the price per bag before you compare quotes. The same logic applies to clothing, where fabric often sets the floor: our guide to minimum order quantities explains how.
Citation Capsule Bag minimums vary by maker and design. Optima Bags states 100 pieces per model, Quanzhou Osgoodway 500 pieces per style and colour, and DANKIN 25 to 1,000 for a custom logo depending on the design; Fieldtex states no minimum order quantities. Custom hardware can carry its own minimum, so ask for tooling to be quoted separately.
What Does a Bag Tech Pack Need That a Garment Tech Pack Doesn't?
Hardware, first. A garment spec can work with a fabric, a colourway, a size chart and stitch notes. A bag quote stalls without a component list, because the components are where much of the cost and lead time sit.
As a minimum, give the base fabric and denier (1000D Cordura behaves very differently from 600D polyester), the lining, the webbing width and grade, the zip brand, gauge and slider, and every buckle, D-ring, grommet and snap by material. Add the load the bag must carry: "a 15-inch laptop plus a day's kit" tells the maker where to reinforce; "make it strong" does not.
Plan the decoration early as well. Logos are often embroidered or printed on flat panels before the bag is sewn, so artwork, placement and thread colours belong in the first version of the spec. Some makers prefer to develop the spec with you: Tough Traveler, for example, says a tech pack is not always useful for its own methods and suggests talking to it first.
How Do You Vet a Bag Manufacturer?
Start with a sample, then test it. A bag's quality sits where a photo can't show it: bar-tacked strap anchors, box-stitched handles, bound internal seams, zip gauge and buckle grade. Load it beyond the weight it should carry, use it for a week and check every seam you can reach.
Then read the maker's own pages. A real bag factory lists bag fabrics and hardware; a clothing factory lists jersey and French terry and may pass your bag to someone else. Ask whether production happens in the maker's own facility or with partners, as Osgoodway says it uses both. Ask for certificate numbers for any audit or certification it lists, and check them. Our article on red flags when choosing a manufacturer covers the general checks, which apply to bag makers too.
Making clothing as well? Our team places and manages apparel production in Portugal from 100 units per style. Get in contact and we reply within 24 hours, or browse the factory directory (€49).
Where Does Portugal Clothing Factory Fit?
We don't make bags. Our team places and manages clothing production with partner factories in northern Portugal, and our services page lists footwear, bags and other hard goods as outside what we do. For a bag, contact a specialist maker like the ones above.
Many brands that add bags also make clothing, and that part we can help with: t-shirts, hoodies, knitwear, wovens and outerwear, from 100 units per style (sometimes 50 for basics, decided with the factory). If you are choosing between buying finished blanks and developing your own garment, read cut-and-sew vs blanks, and for how to approach any manufacturer, our guide to finding a clothing manufacturer.
Frequently Asked Questions About Bag Manufacturers
Can my clothing manufacturer also make bags?
Usually not. A bag line runs heavy-duty and walking-foot machines that feed thick fabrics such as 1000D Cordura, ballistic nylon and heavy canvas, and it keeps hardware such as webbing, grommets, D-rings and buckles. Most apparel factories have neither. If a clothing factory says yes to a bag order, ask whether the bag will be made on its own premises or sent to another plant.
What is the minimum order for custom bags?
It varies by maker and by design. Of the seven makers in this guide, Optima Bags states 100 pieces per model, Quanzhou Osgoodway 500 pieces per style and colour, and DANKIN 25 to 500 or 1,000 pieces for a custom logo, depending on the design. Fieldtex states no minimum order quantities, and Tough Traveler works from a single prototype to runs of thousands. Custom hardware can carry its own minimum, so ask for it separately.
Where are most bags manufactured?
By volume, in Asia. IndexBox reports that the United States imported 246 million units of handbags in 2024, and that China (93 million), Cambodia (50 million) and Vietnam (17 million) supplied a combined 71% of that volume. By value the order changes: Italy led at $1.2 billion, ahead of Cambodia and China.
Are any bags still made in the USA?
Yes. Unionwear makes custom union-made bags at its factory in Newark, New Jersey; Fieldtex Cases makes tactical, medical and industrial bags in Rochester, New York; Tough Traveler has made bags in the USA since 1970; and John Boyt Industrial Sewing in Urbandale, Iowa, sews custom bags on contract. Expect a higher price per bag than high-volume production in Asia.
Does Portugal Clothing Factory make bags?
No. Our team places and manages clothing production with partner factories in northern Portugal, and our services page lists bags as outside what we do. If your range also includes apparel, such as t-shirts, hoodies or outerwear, we can help with that part.
We work with 80+ documented Portuguese clothing factories in the northern textile cluster. Tell us your garment, volume, and timeline; our team replies within 24 hours. If it is a fit, we place and manage your production with the partner factory built for it. Fee quoted in writing, no commissions.
Get in contact Download the directory (€49)Need a tech pack for a garment? Get a factory-ready single-style tech pack for €79. See what's included.
Sources used in this article
- IndexBox, Handbags United States market overview 2024: 246M units, $3.9B; China, Cambodia, Vietnam by units; Italy, Cambodia, China by value.
- Unionwear, Custom backpacks: 100% custom made in USA at the Newark, NJ factory; since 1992.
- Fieldtex Cases, Military-grade sewing: since 1973, ISO 9001, 86,000 sq ft, 125+ operators, Berry Amendment, no minimum order quantities.
- Tough Traveler, Custom design services: made in USA since 1970, in-house production, prototype costs, decoration quantities.
- John Boyt Industrial Sewing, Custom bags: processes, materials, hardware, example volume.
- Quanzhou Osgoodway, About: since 2014, factory size, partner network, MOQ, certifications.
- DANKIN Light Industrial: founded 1991, production lines, workers, audits, custom-logo MOQ.
- Optima Bags, About and Backpack manufacturer: history, Kundli factory, certifications, MOQ.
Portugal Clothing Factory is a group of documented Portuguese clothing factories in the northern textile cluster (Porto, Guimarães, Braga, Barcelos, Famalicão). We quote our fee in writing, reply within 24 hours, and place and manage production with the factory in our group built for your product. See how we work or get in contact.